Quick Answer
A go no-go gauge is a fixed-size attribute gauge that answers one question: is this feature inside its limits? The go end is made to the maximum-material limit and has to enter or fit; the no-go end is made to the least-material limit and has to stop. Gauging is the fastest way to accept or reject a hole, a shaft or a thread on the shop floor. What it does not do is report a size.
Key Takeaways
- A go no-go gauge returns a pass or fail decision, not a dimension, so it cannot show how far a part sits from a limit.
- The go member checks the maximum-material size; the no-go member checks the least-material size.
- Plug gauges check internal features; ring and snap gauges check external ones; thread gauges check the thread envelope.
- Gauge limits follow the drawing limits, with gauge tolerance and a wear allowance taken from the part tolerance.
- Attribute gauging is fast per part; variable measurement is slower but gives trendable numbers.
What a Go No-Go Gauge Actually Checks
A plain go no-go gauge checks size, and nothing else. Take a bore with a drawing limit of 10.00 to 10.10 mm. The go end of a plug gauge is made to the low limit, the smallest hole the drawing allows, and it has to pass through. If it enters, the hole is at or above the minimum size. The no-go end is made to the high limit and has to stop at the entry — a complete answer about size, with no reading and no trend.
Geometry is a separate question. A plain gauge cannot check position, perpendicularity or a hole pattern, because those are relationships between features rather than one size. They are proved with a functional gauge built to virtual condition, or with a coordinate measuring machine. Where a drawing mixes size and position on the same hole, settle up front which method proves which; the position tolerance guide for hole patterns works through it.
Plug, Ring and Thread Gauges
The family splits by the feature it touches:
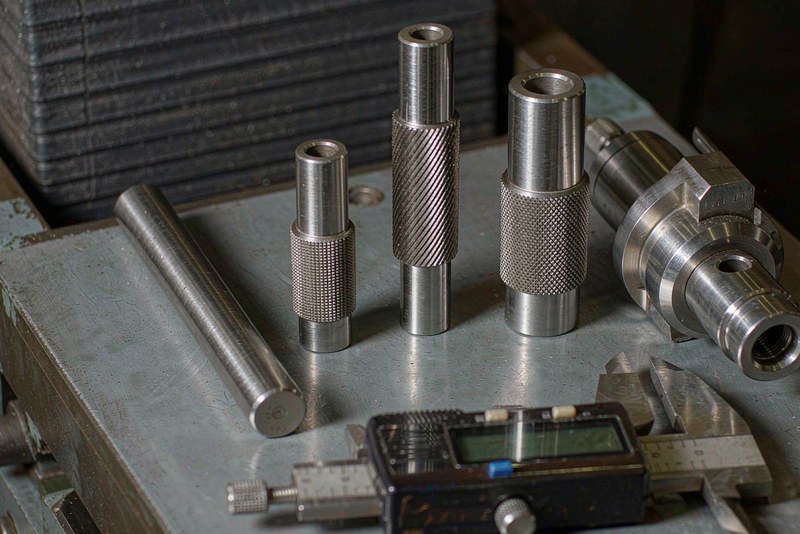
- Plain plug gauge — a cylindrical go/no-go pair, usually double-ended, for internal diameters.
- Ring gauge — go and no-go members for external diameters such as shafts and pins.
- Thread plug gauge — proves the functional envelope of an internal thread; the no-go member is tried a few turns.
- Functional or receiver gauge — a plate with pins at virtual condition, for a hole pattern.
A thread plug gauge confirms that a mating screw will assemble, but it does not report where the pitch diameter sits inside its band. Where pitch diameter is critical, that is a measurement job; hole tolerances and fits for CNC parts covers the same logic for plain bores.
Gauge Tolerance and Wear Allowance
A gauge is not a copy of the drawing limit. It is a manufactured object whose own tolerance has to live inside the part tolerance. The governing gauge standard assigns a gauge tolerance, typically a modest fraction of the part tolerance, plus a wear allowance on the member that touches every accepted piece. The effect is a guard band: the gauge accepts a slightly tighter band than the drawing limits, so a part that passes sits comfortably inside the limit rather than on it.
Boundary parts deserve a decision. A feature sitting exactly on the drawing limit can fail a gauge that carries a wear allowance or that has already worn. Where the boundary matters — a press fit, a bearing seat, a sealing bore — say so on the drawing or agree the acceptance method.
| Question | Attribute gauge (go/no-go) | Variable measurement (bore gauge, micrometer, CMM) |
|---|---|---|
| Answer it gives | Pass or fail | A number with uncertainty |
| Time per feature | Seconds | Minutes |
| Data for trending | None | Full |
| Typical use | Full check of a stable process | Capability studies and first-off approval |
When a Go No-Go Gauge Beats a CMM or a Caliper
A CMM and a go no-go gauge answer different questions. The gauge wins when the question is whether one part is acceptable on a feature you intend to check on every piece. It takes seconds, needs no programming, and the operator cannot drift into another datum scheme mid-shift.
Measurement wins when process capability is the question: numbers can be plotted, so drift shows up before it reaches a limit. Attribute gauging produces no data, which makes an unstable process a poor place to start with a gauge.
The mixed route is common: measure the first-off part and the first article, confirm the process is centred, then gauge the run with a sampling plan for measurement. The in-process inspection overview covers where that sampling belongs.
Common Mistakes When Gauging
- Forcing the no-go end. If it needs pressure to enter, the part fails; insertion force is not a criterion.
- Gauging a warm part. A bore straight off the machine has not reached room temperature.
- Ignoring the edge condition. A burr at the entry can stop a go gauge the bore itself would pass, so agree whether gauging happens before or after deburring.
- Ordering to the nominal size instead of the drawing limits, or assuming one gauge covers a whole hole pattern.
What to Put on the Drawing and the Gauge Order
On the drawing, state the requirement rather than the apparatus. A diameter with limits, a thread callout and a position tolerance are requirements; "check with a go/no-go gauge" is a method, and it belongs in a note once you and the supplier have agreed it. First article inspection is the natural place to settle that method before a run starts, because both sides confirm there how each requirement will be proved.
When you order gauges, ask for four things: the limits the gauge was made to, the gauge tolerance class, the master used to certify it, and the recertification interval the maker recommends.
FAQ
Does a go no-go gauge tell you the size of a hole?
No. It tells you whether the hole is inside its limits. Where a number is needed, use a bore gauge, a micrometer or a CMM.
Can a go no-go gauge replace a CMM?
For one size on a stable process it can carry acceptance. It cannot check position, form or a pattern, so a CMM is still needed for those.
How often should plug gauges be recertified?
It depends on usage and material. Gauging abrasive material in volume calls for shorter intervals. Follow the maker's recommendation and your own wear records.